
Are stringent Zero Liquid Discharge (ZLD) mandates, extreme space constraints, failing conventional clarifiers, or the need for ultra-pure recycled water causing operational headaches for your facility? As a premier STP Plant with MBR Technology Manufacturer, Ventilair Engineers Pvt Ltd delivers high-performance, next-generation Membrane Bioreactor (MBR) Sewage Treatment Plants engineered to provide unparalleled effluent clarity and maximum water recovery in a fraction of the traditional footprint.
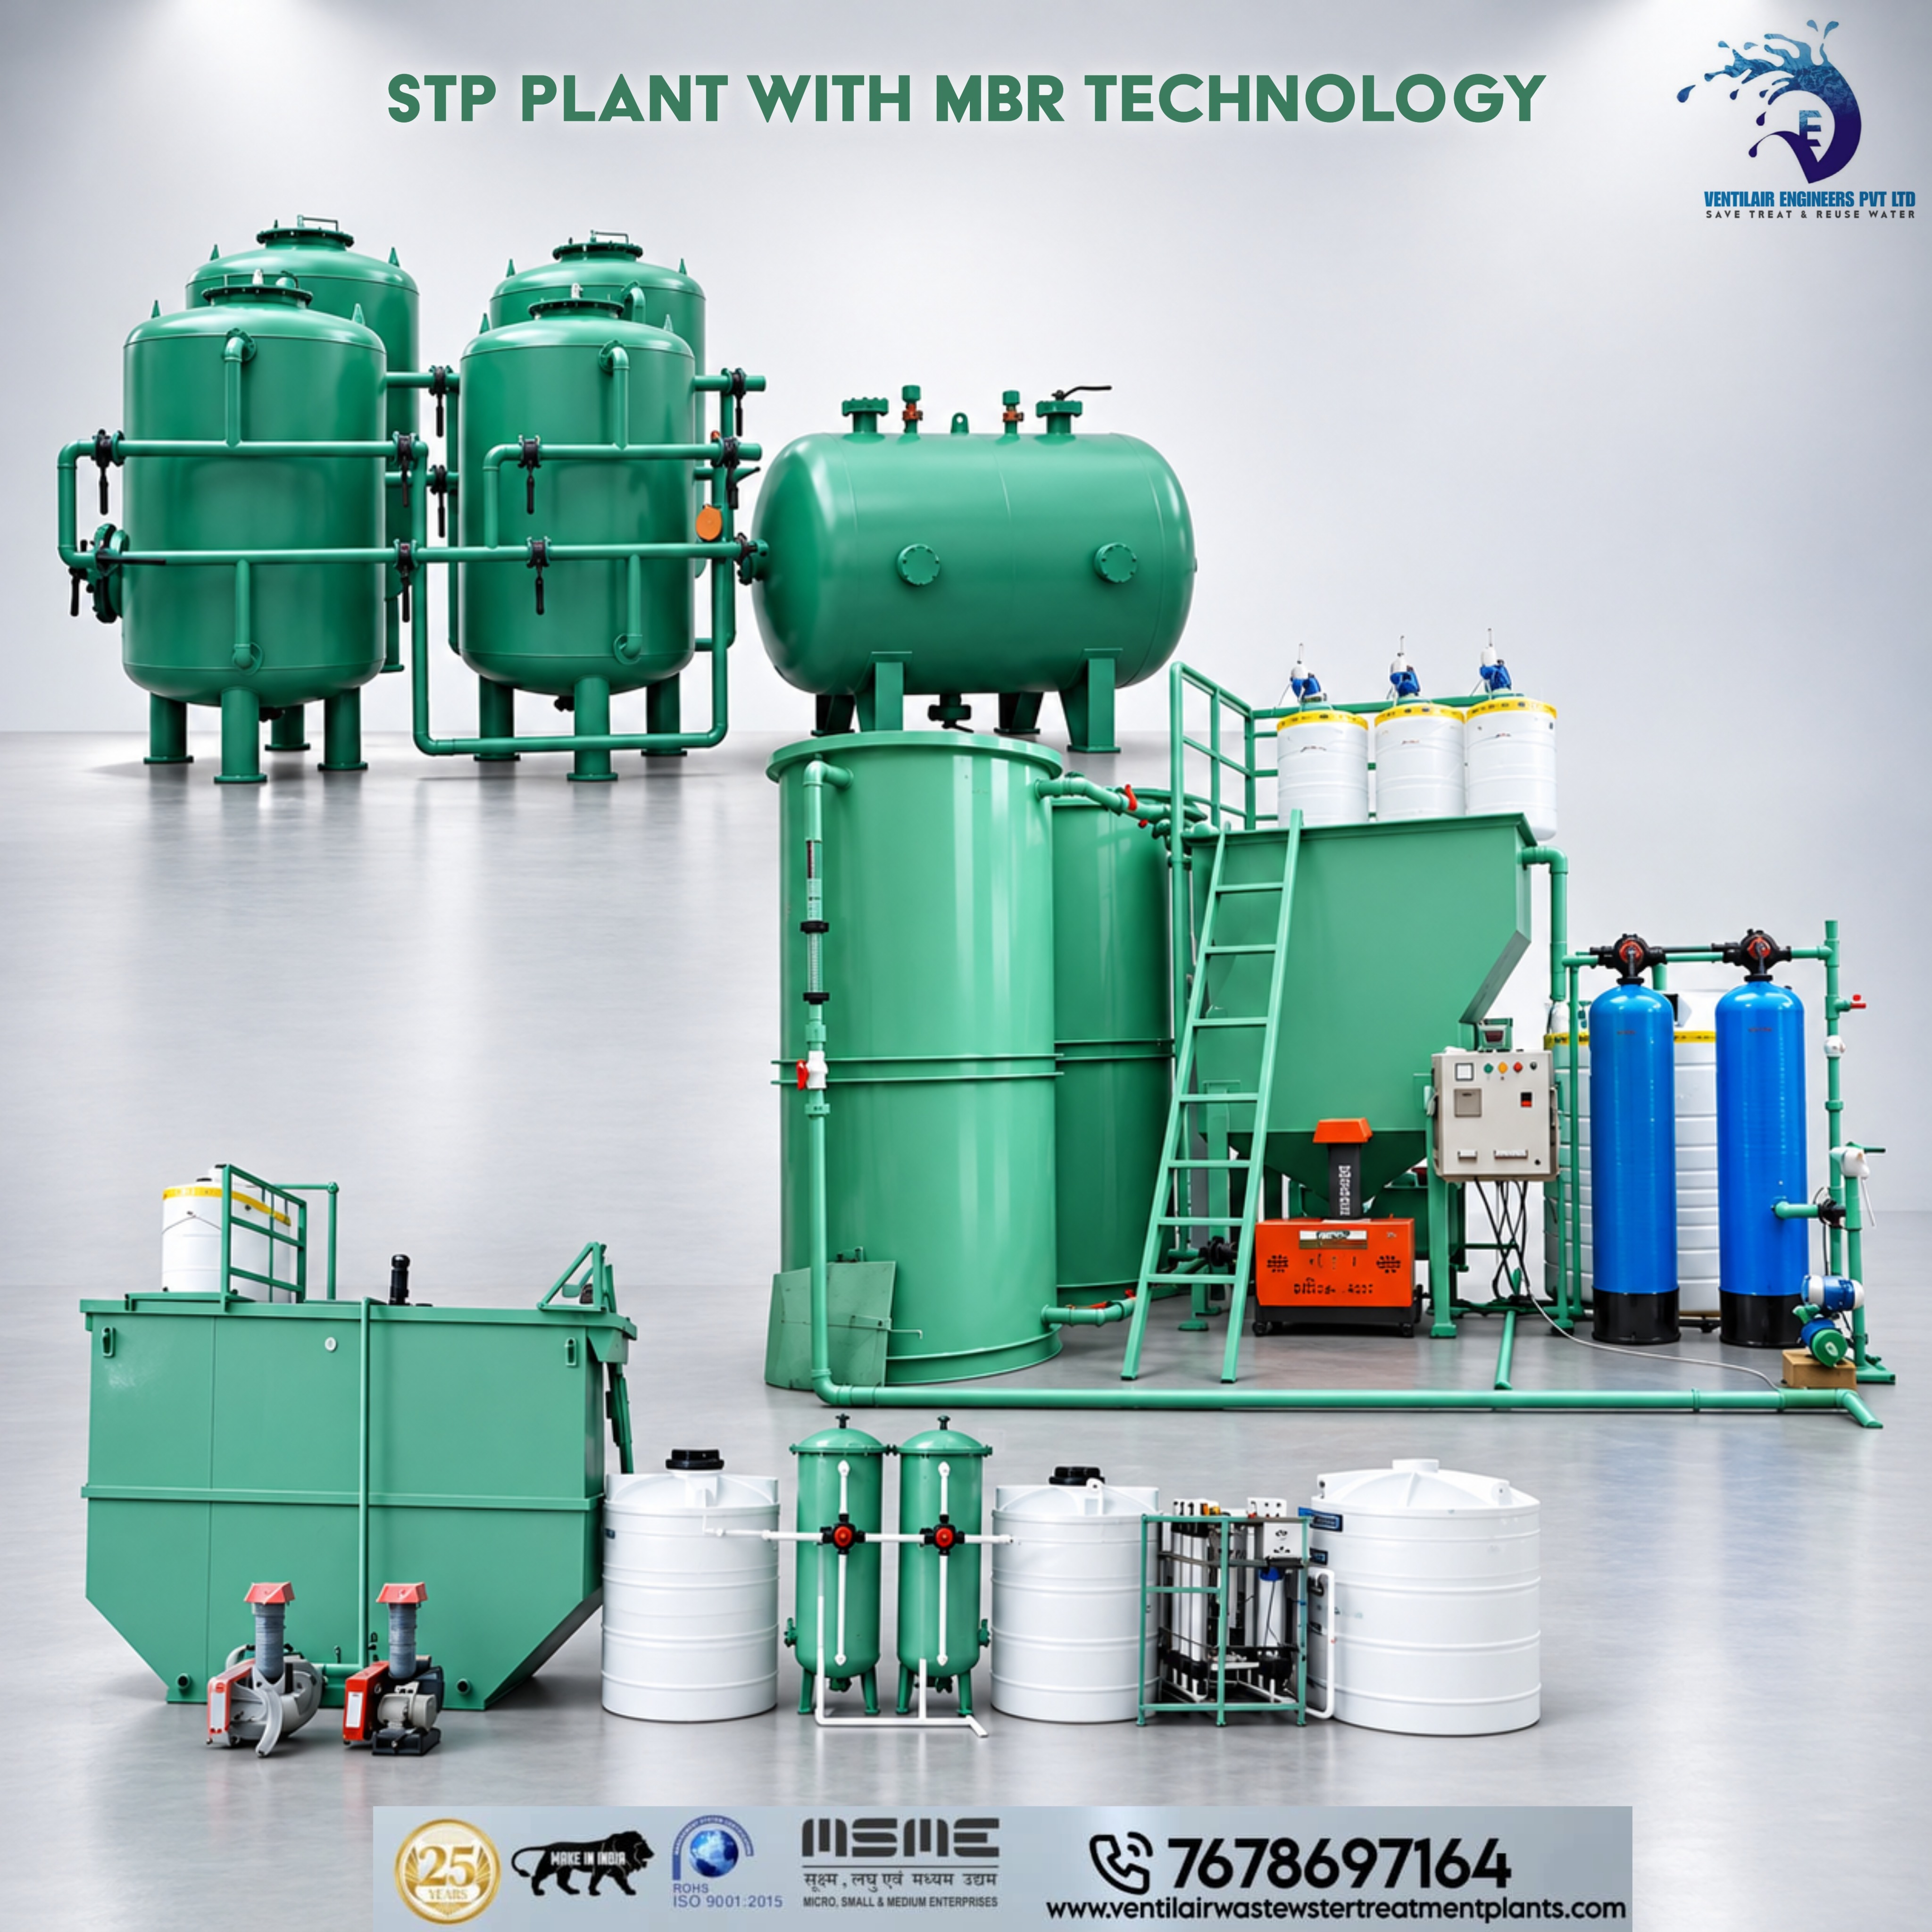
Conventional wastewater setups rely on large settling clarifiers and often struggle to consistently meet strict discharge parameters under fluctuating loads. MBR technology revolutionizes this by directly integrating advanced ultrafiltration membranes with the biological aerobic process, completely eliminating the need for secondary clarification. As showcased in 40.jpg, our advanced, pre-engineered MBR platform ensures complete retention of biomass, resulting in a highly concentrated mixed liquor that aggressively breaks down organic loads and delivers crystal-clear, pathogen-free water ready for high-end reuse.
Key Engineering Highlights of Ventilair’s MBR STP Plants:
💧 Ultra-Pure, Pathogen-Free Effluent: Advanced membrane microfiltration acts as an absolute physical barrier against suspended solids, bacteria, and turbidity, producing superior quality water ideal for HVAC cooling towers, dual plumbing, and industrial process reuse.
🏗️ Ultra-Compact & Space-Optimized Design: By eliminating bulky secondary clarifiers and operating at high biomass concentrations (MLSS), our MBR systems require a significantly smaller civil footprint, making them perfect for premium high-rises and tight basement utilities.
📉 Consistent Performance & Low Sludge Yield: Delivers stable, highly reliable treatment even during shock hydraulic surges, while generating substantially less waste sludge compared to conventional activated sludge processes.
📜 100% Pollution Control Board & ZLD Compliance: Tailored to help modern industries, commercial complexes, and real estate developers effortlessly exceed the most rigid recycling and discharge guidelines enforced by state watchdogs like DPCC, HSPCB, and UPPCB.
🏆 25+ Years of Trust as a Premium Manufacturer: Fabricated strictly to robust “Make in India“ durability benchmarks by an ISO 9001:2015 and MSME certified industry leader, ensuring minimal maintenance overheads and maximum operational runtime.
📍 Turnkey Installation & Maintenance Services Across Key Development Hubs:
Delhi Clusters: Okhla Industrial Area, Bawana, Narela, Mayapuri, Patparganj, Mangolpuri, and Lawrence Road.
Haryana Belts: Gurugram (Gurgaon), IMT Manesar, IMT Kharkhoda Industrial Area, Sonipat, Kundli, Rai, Murthal, Barhi, and Faridabad.
Uttar Pradesh Zones: Noida (Sector 63, Sector 58, Phase-II, Phase-III), Greater Noida (Ecotech zones), Ghaziabad, and Sahibabad Industrial Area.
Upgrade to next-generation membrane technology, maximize your water recycling potential, and partner with a trusted manufacturer to maintain absolute regulatory compliance. Contact our specialized industrial water engineering division today to get a custom technical MBR layout or request an on-site project estimation.
✨ Ventilair Engineers – Advanced Engineering. Pure Water Solutions. Complete Compliance.
#MBRTechnology #MBRSTP #MembraneBioreactor #STPPlantManufacturer #SewageTreatmentPlant #WastewaterTreatmentPlant #ZeroLiquidDischarge #WaterRecycling #Ultrafiltration #BODReduction #CODReduction #WaterEngineering #OkhlaIndustrial #BawanaIndustrial #NoidaIndustrial #GurgaonIndustrial #IMTManesar #IMTKharkhoda #SonipatIndustrial #FaridabadIndustrial #PollutionCompliance #DPCC #HSPCB #UPPCB #VentilairEngineers #MakeInIndia #WaterReuse